EOS NickelAlloy IN718
Material Data Sheet | Powder Product No. 9011-0020 / 9030-0022
EOS NickelAlloy IN718
High Temperature Strength and Corrosion Resistance
EOS NickelAlloy IN718 is a precipitation-hardening nickel-chromium alloy that is characterized by having good tensile, fatigue, creep and rupture strength at temperatures up to 700 °C (1290 °F). Parts built from EOS NickelAlloy IN718 can be easily post-hardened by precipitation-hardening heat treatments.
EOS NickelAlloy IN718 is a nickel alloy powder intended for manufacturing parts on EOS metal systems with EOS DMLS processes.
- Good tensile, fatigue, creep and rupture strength at temperatures up to 700 °C (1 290 °F)
- Parts are easily precipitation hardened
- Parts can be machined, spark-eroded, welded, micro shot-peened, polished and coated in both as-built and age-hardened states
- Available in 10 kg drum and 500 kg Big Bag packaging
- Gas turbine components
- Instrumentation parts
- Power industry parts
- Process industry parts
The EOS Quality Triangle
EOS incorporates these TRLs into the following two categories:
- Premium products (TRL 7-9): offer highly validated data, proven capability and reproducible part properties.
- Core products (TRL 3 and 5): enable early customer access to newest technology still under development and are therefore less mature with less data.
All of the data stated in this material data sheet is produced according to EOS Quality Management System and international standards
POWDER PROPERTIES
The chemical composition of EOS NickelAlloy IN718 is in compliance with UNS N07718, AMS 5662, AMS 5664, W.Nr 2.4668, DIN NiCr19Fe19NbMo3.
Powder Chemical Composition (wt.-%)
| Element | Min. | Max. |
|---|---|---|
| Fe | Balance | |
| Ni | 50 | 55 |
| Cr | 17 | 21 |
| Nb | 4.75 | 5.5 |
| Mo | 2.8 | 3.3 |
| Ti | 0.65 | 1.15 |
| Al | 0.2 | 0.8 |
| Co | 0 | 1 |
| Cu | 0 | 0.3 |
| Si | 0 | 0.35 |
| Mn | 0 | 0.35 |
| Ta | 0 | 0.05 |
| C | 0 | 0.08 |
| S | 0 | 0.015 |
| P | 0 | 0.015 |
| B | 0 | 0.006 |
| Pb | 0 | 0.0005 |
| Se | 0 | 0.002 |
| Bi | 0 | 0.00003 |
Powder Particle Size
| Generic Particle Size Distribution | 20 - 55 µm | |
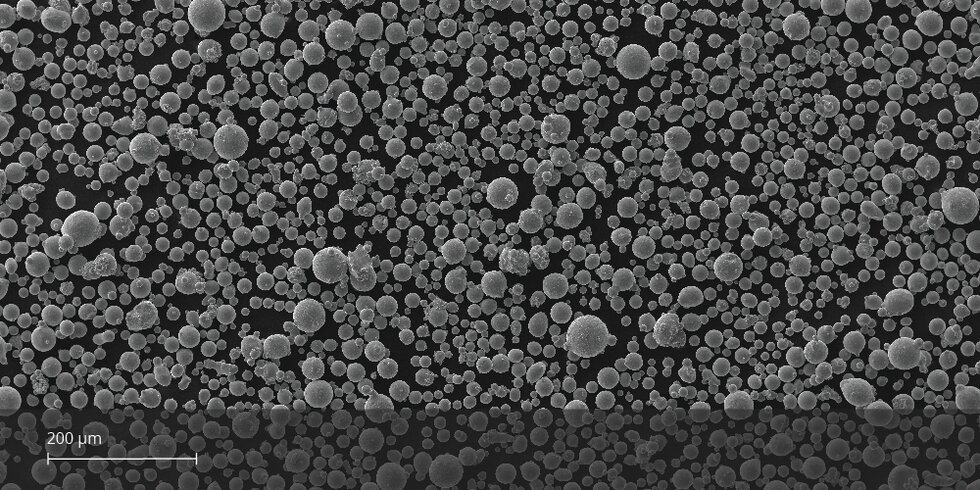
SEM micrograph of EOS NickelAlloy IN718 powder
HEAT TREATMENT
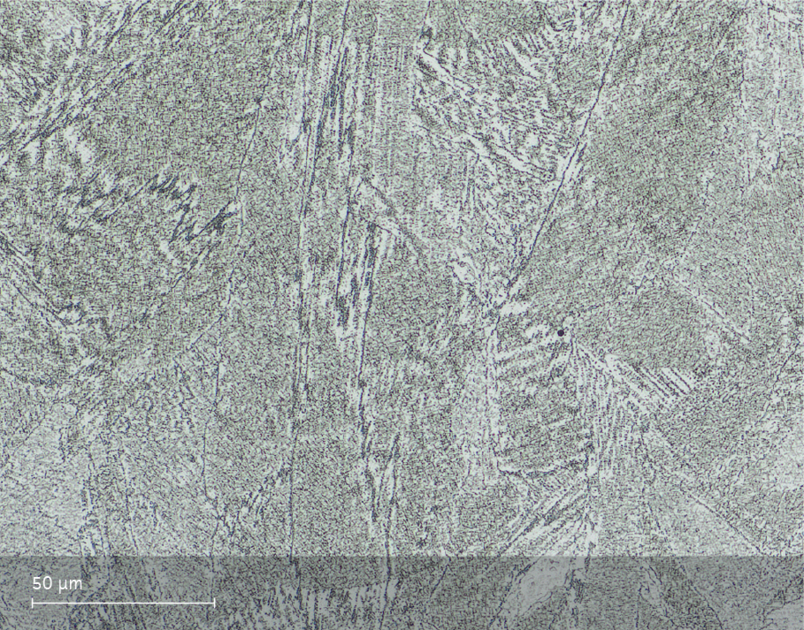
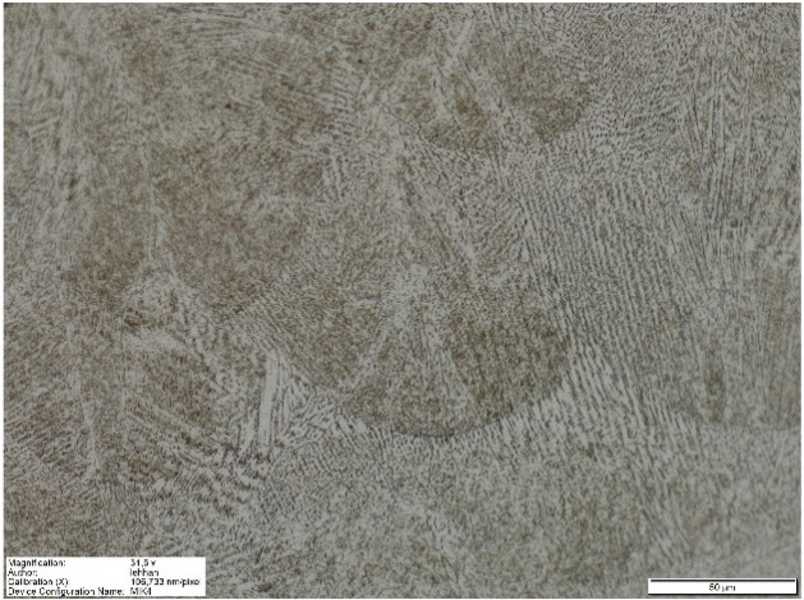
Heat treatment procedure conform to Aerospace Material Specification AMS 2774 and AMS 5662. As manufactured microstructure for additively manufactured IN718 consists of gamma phase (γ). Heat treatment for IN718 is required to produce desired microstructure and part properties (gamma double prime precipitates, γ“). Heat treatment is also used to relieve stresses
Step 1: Solution Annealing: hold at 954 °C (1 750 °F ) for 1 hour per 25 mm (0.98 inch) of thickness, air (/argon) cool
Step 2: Ageing Treatment: hold at 718 °C (1 325 °F ) 8 hours, furnace cool to 621 °C (1 150 °F ) and hold at 621 °C (1 150 °F ) for total precipitation time of 18 hours, air (/argon) cool
| System Setup | EOS M 400 |
|---|---|
| EOS Material set | IN718_040_FlexM400 |
| Powder Product No. | 9011-0020 / 9030-0022 |
| Software Requirements |
EOSPRINT 2.5 or newer |
| Recoater Blade | HSS (High Speed Steel) |
| Inert gas | Argon |
| Sieve | 63 µm |
| Additional Information | |
|---|---|
| Layer Thickness | 40 µm |
| Volume Rate | 4.2 mm³/s |
Microstructure of the Produced Parts
| Defects | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Defect Percentage | 40 µm | 0.02 % | - |
| Density EN ISO 3369 | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Density | 40 µm | ≥ 8.15 g/cm³ | - |
Mechanical Properties Heat Treated
| EN ISO 6892-1 Room Temperature | 40 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 1150 | 1420 | 16 | - | - | - |
| Horizontal | 1240 | 1510 | 14 | - | - | - |
Heat treatment procedure conform to Aerospace Material Specification AMS 2774 and AMS 5662.
As manufactured microstructure for additively manufactured IN718 consists of gamma phase (γ). Heat treatment for IN718 is required to produce desired microstructure and part properties (gamma double prime precipitates, γ"). Heat treatment is also used to relieve stresses.
Step 1:
Solution Anneal: hold at 954 °C (1750 °F ) for 1 hour per 25mm (0.98 inch) of thickness, air (/argon) cool
Step 2:
Ageing treatment; hold at 718 °C (1325 °F ) 8 hours, furnace cool to 621 °C (1150 °F ) and hold at 621 °C (1150 °F ) for total precipitation time of 18 hours, air (/argon) cool
Mechanical Properties As Manufactured
| EN ISO 6892-1 Room Temperature | 40 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 650 | 1000 | 29 | - | - | - |
| Horizontal | 780 | 1090 | 24 | - | - | - |
Surface Roughness
| Surface Roughness | From | To |
|---|---|---|
| Sa (µm) | - | - |
| Ra (µm) | - | - |
| System Setup | EOS M 400-4 |
|---|---|
| EOS Material set | IN718_040_FlexM404 |
| Powder Product No. | 9011-0020 / 9030-0022 |
| Software Requirements |
EOSPRINT 2.0 or newer |
| Recoater Blade | HSS (High Speed Steel) |
| Inert gas | Argon |
| Sieve | 63 µm |
| Additional Information | |
|---|---|
| Layer Thickness | 40 µm |
| Volume Rate | up to 4 x 4.2 mm³/s |
| Min. Wall Thickness | typical 0.3 - 0.4 mm |
Microstructure of the Produced Parts
| Defects | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Defect Percentage | 40 µm | 0.04 % | - |
| Density EN ISO 3369 | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Density | 40 µm | ≥ 8.15 g/cm³ | - |
Mechanical Properties Heat Treated
| EN ISO 6892-1 Room Temperature | 40 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 1220 | 1420 | 16 | - | - | - |
| Horizontal | 1300 | 1510 | 15 | - | - | - |
Heat treatment procedure conform to Aerospace Material Specification AMS 2774 and AMS 5662.
As manufactured microstructure for additively manufactured IN718 consists of gamma phase (γ). Heat treatment for IN718 is required to produce desired microstructure and part properties (gamma double prime precipitates, γ"). Heat treatment is also used to relieve stresses.
Step 1:
Solution Anneal: hold at 954 °C (1750 °F ) for 1 hour per 25mm (0.98 inch) of thickness, air (/argon) cool
Step 2:
Ageing treatment; hold at 718 °C (1325 °F ) 8 hours, furnace cool to 621 °C (1150 °F ) and hold at 621 °C (1150 °F ) for total precipitation time of 18 hours, air (/argon) cool
Surface Roughness
| Surface Roughness | From | To |
|---|---|---|
| Sa (µm) | - | - |
| Ra (µm) | 4.5 | - |
| System Setup | EOS M 290 |
|---|---|
| EOS Material set | IN718_040_PerformanceM291 |
| Powder Product No. | 9011-0020 / 9030-0022 |
| Software Requirements |
EOSPRINT 1.7 or newer EOSPRINT 2.6 or newer and EOSYSTEM 2.9 or newer |
| Recoater Blade | HSS (High Speed Steel) |
| Nozzle | EOS Grid Nozzle |
| Inert gas | Argon |
| Sieve | 63 µm |
| Additional Information | |
|---|---|
| Layer Thickness | 40 µm |
| Volume Rate | 4.2 mm³/s |
| Min. Wall Thickness | 0.3 - 0.4 mm |
Chemical and Physical Properties of Parts
Microstructure of the Produced Parts
| Defects | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Defect Percentage | 40 µm | 0.03 % | - |
| Density EN ISO 3369 | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Density | 40 µm | ≥ 8.15 g/cm³ | - |
Mechanical Properties Heat Treated
| Room Temperature | | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
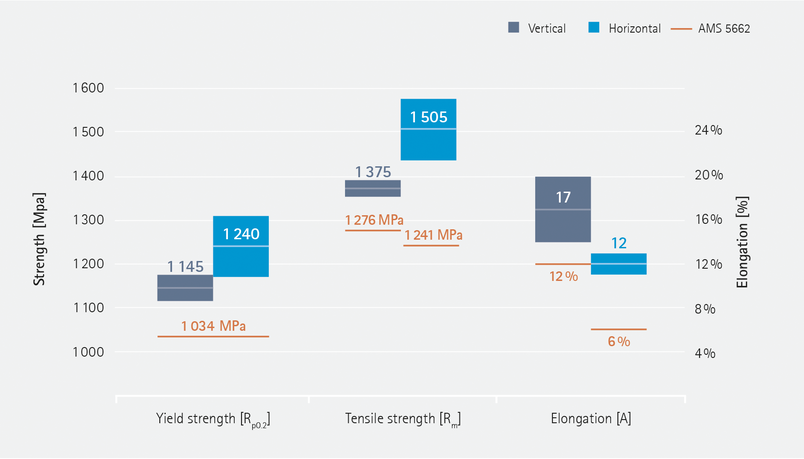
| Vertical | 1145 | 1375 | 17 | - | - | - |
| Horizontal | 1240 | 1505 | 12 | - | - | - |
Heat treatment procedure conform to Aerospace Material Specification AMS 2774 and AMS 5662.
As manufactured microstructure for additively manufactured IN718 consists of gamma phase (γ). Heat treatment for IN718 is required to produce desired microstructure and part properties (gamma double prime precipitates, γ"). Heat treatment is also used to relieve stresses.
Step 1:
Solution Anneal: hold at 954 °C (1750 °F ) for 1 hour per 25mm (0.98 inch) of thickness, air (/argon) cool
Step 2:
Ageing treatment; hold at 718 °C (1325 °F ) 8 hours, furnace cool to 621 °C (1150 °F ) and hold at 621 °C (1150 °F ) for total precipitation time of 18 hours, air (/argon) cool
Mechanical Properties As Manufactured
| EN ISO 6892-1 Room Temperature | 40 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 650 | 970 | 32 | - | - | - |
| Horizontal | 800 | 1090 | 25 | - | - | - |
Hardness
| Heat Treated | |
|---|---|
| Value | 47 |
| Unit | HRC |
| Heat Treated | |
|---|---|
| Value | 466 |
| Unit | HB |
Surface Roughness
| Surface Roughness | From | To |
|---|---|---|
| Sa (µm) | - | - |
| Ra (µm) | - | - |
Coefficient of Thermal Expansion
| Temperature | |
|---|---|
| 13.1*10-6/K | 25 – 100 ºC |
| 13.7*10-6/K | 25 – 200 ºC |
| 14.1*10-6/K | 25 – 300 ºC |
| 14.4*10-6/K | 25 – 400 ºC |
| 14.7*10-6/K | 25 – 500 ºC |
| 15*10-6/K | 25 – 600 ºC |
| 15.5*10-6/K | 25 – 700 ºC |
| System Setup | EOS M 300-4 |
|---|---|
| EOS Material set | IN718_040_CoreM304 |
| Powder Product No. | 9011-0020 / 9030-0022 |
| Software Requirements |
EOSPRINT 2.9 or newer |
| Recoater Blade | HSS (High Speed Steel) |
| Inert gas | Argon |
| Sieve | 63 µm |
| Additional Information | |
|---|---|
| Layer Thickness | 40 µm |
| Volume Rate | up to 4 x 4.2 mm³/s |
Microstructure of the Produced Parts
| Defects | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Defect Percentage | 40 µm | < 0.05 % | - |
Mechanical Properties
Mechanical Properties As Manufactured
| EN ISO 6892-1 Room Temperature | 40 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 635 | 955 | 36 | - | - | - |
| Horizontal | 795 | 1090 | 27 | - | - | - |
Mechanical Properties Heat Treated
| EN ISO 6892-1 Room Temperature | 40 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 1140 | 1370 | 20 | - | - | - |
| Horizontal | 1270 | 1530 | 15 | - | - | - |
Heat treatment procedure conform to Aerospace Material Specification AMS 2774 and AMS 5662.
As manufactured microstructure for additively manufactured IN718 consists of gamma phase (γ). Heat treatment for IN718 is required to produce desired microstructure and part properties (gamma double prime precipitates, γ"). Heat treatment is also used to relieve stresses.
Step 1:
Solution Anneal: hold at 954 °C (1750 °F ) for 1 hour per 25mm (0.98 inch) of thickness, air (/argon) cool
Step 2:
Ageing treatment; hold at 718 °C (1325 °F ) 8 hours, furnace cool to 621 °C (1150 °F ) and hold at 621 °C (1150 °F ) for total precipitation time of 18 hours, air (/argon) cool
Surface Roughness
| Surface Roughness | From | To |
|---|---|---|
| Sa (µm) | - | - |
| Ra (µm) | - | - |
| System Setup | EOS M 300-4 |
|---|---|
| EOS Material set | IN718_080_HiProM304 |
| Powder Product No. | 9011-0020 / 9030-0022 |
| Software Requirements |
EOSPRINT 2.11 or newer |
| Recoater Blade | HSS (High Speed Steel) |
| Inert gas | Argon |
| Additional Information | |
|---|---|
| Layer Thickness | 80 µm |
| Volume Rate | up to 4 x 9.9 mm³/s |
| Min. Wall Thickness | 0.3 - 0.4 mm |
Chemical and Physical Properties of Parts
Microstructure of the Produced Parts
| Defects | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Defect Percentage | 80 µm | 0.03 % | - |
| Density EN ISO 3369 | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Density | 80 µm | ≥ 8.15 g/cm³ | - |
Mechanical Properties Heat Treated
| EN ISO 6892-1 Room Temperature | 80 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
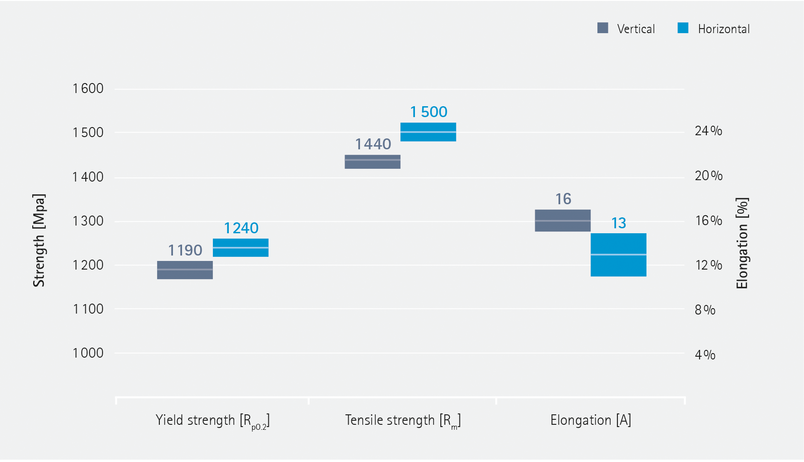
| Vertical | 1190 | 1440 | 16 | - | - | - |
| Horizontal | 1240 | 1500 | 13 | - | - | - |
Heat treatment procedure conform to Aerospace Material Specification AMS 2774 and AMS 5662.
As manufactured microstructure for additively manufactured IN718 consists of gamma phase (γ). Heat treatment for IN718 is required to produce desired microstructure and part properties (gamma double prime precipitates, γ"). Heat treatment is also used to relieve stresses.
Step 1:
Solution Anneal: hold at 954 °C (1750 °F ) for 1 hour per 25mm (0.98 inch) of thickness, air (/argon) cool
Step 2:
Ageing treatment; hold at 718 °C (1325 °F ) 8 hours, furnace cool to 621 °C (1150 °F ) and hold at 621 °C (1150 °F ) for total precipitation time of 18 hours, air (/argon) cool
Mechanical Properties As Manufactured
| EN ISO 6892-1 Room Temperature | | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 620 | 1070 | 26 | - | - | - |
| Horizontal | 760 | 1000 | 33 | - | - | - |
Hardness
| EN ISO 6507 Heat Treated | |
|---|---|
| Value | 456 |
| Unit | HV |
Surface Roughness
| Surface Roughness | From | To |
|---|---|---|
| Sa (µm) | - | - |
| Ra (µm) | - | - |
Process Information Metal
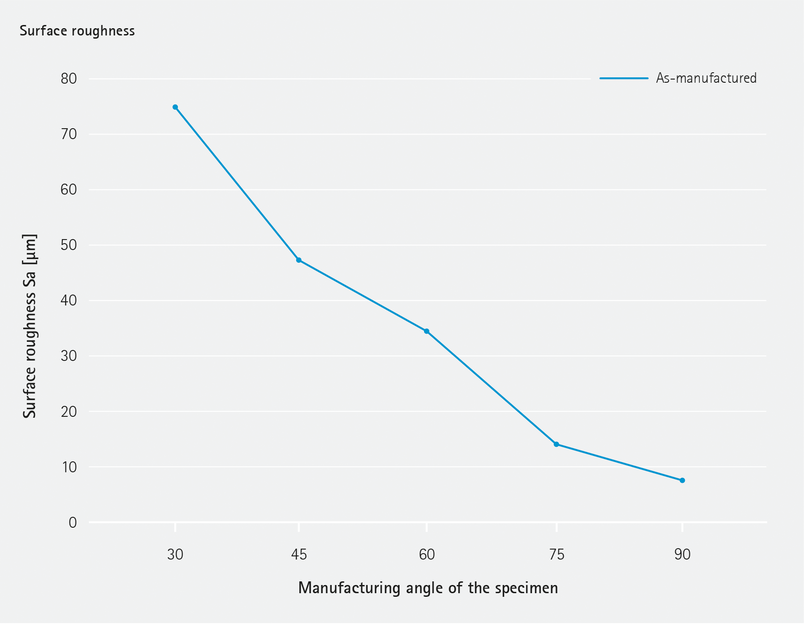
This process parameter includes two variations of the exposure set: the first one provides better productivity while the second one enables low angle buildability down to 20°. The low angle buildability can be optimized further through the part geometry and the length of overhang.
| System Setup | EOS M 400-4 |
|---|---|
| EOS Material set | IN718_040_080_HiProM404 |
| Powder Product No. | 9011-0020 / 9030-0022 |
| Software Requirements |
EOSPRINT 2.11 or newer EOSYSTEM 2.15 or newer |
| Recoater Blade | HSS (High Speed Steel) |
| Nozzle | EOS Aerospike Nozzle |
| Inert gas | Argon |
| Sieve | 63 µm |
| Additional Information | |
|---|---|
| Layer Thickness | 40 µm |
| Volume Rate | up to 4 x 5.2 mm³/s |
| Min. Wall Thickness | typical 0.3 - 0.4 mm |
Chemical and Physical Properties of Parts
Microstructure of the Produced Parts
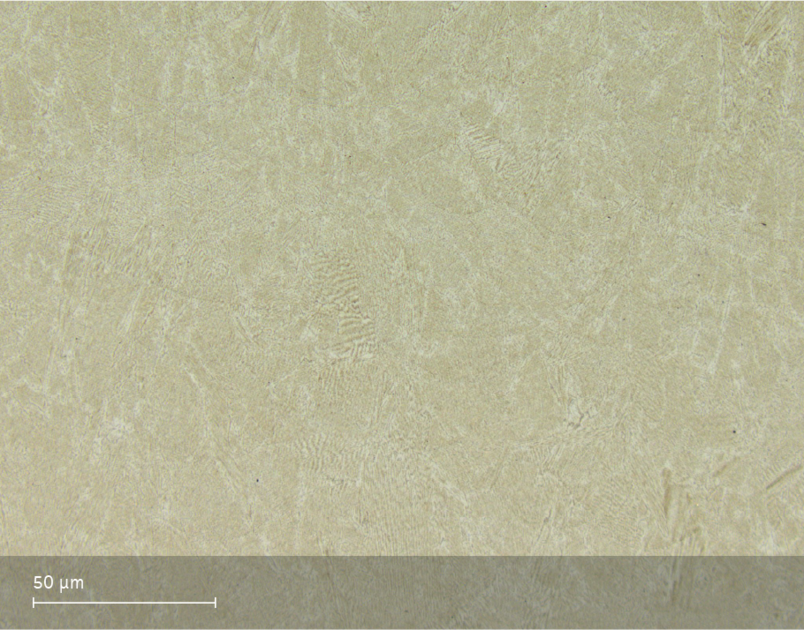
| Defects | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Defect Percentage | 40 µm | 0.01 % | - |
| Density EN ISO 3369 | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Density | 40 µm | ≥ 8.21 g/cm³ | - |
Mechanical Properties Heat Treated
| EN ISO 6892-1 Room Temperature | 40 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
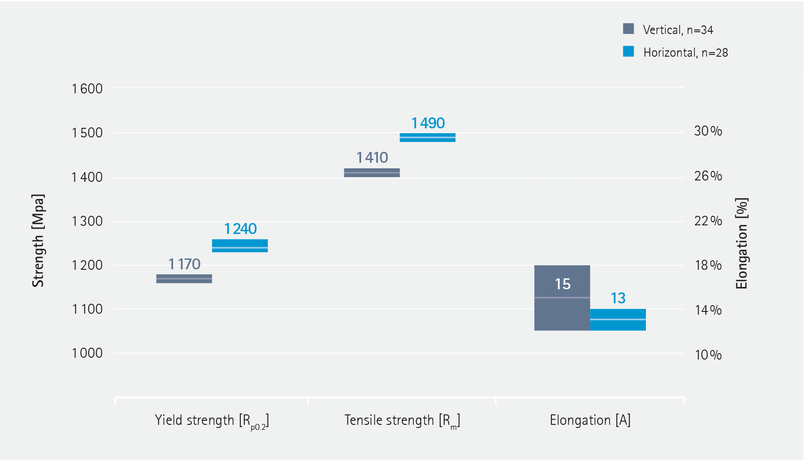
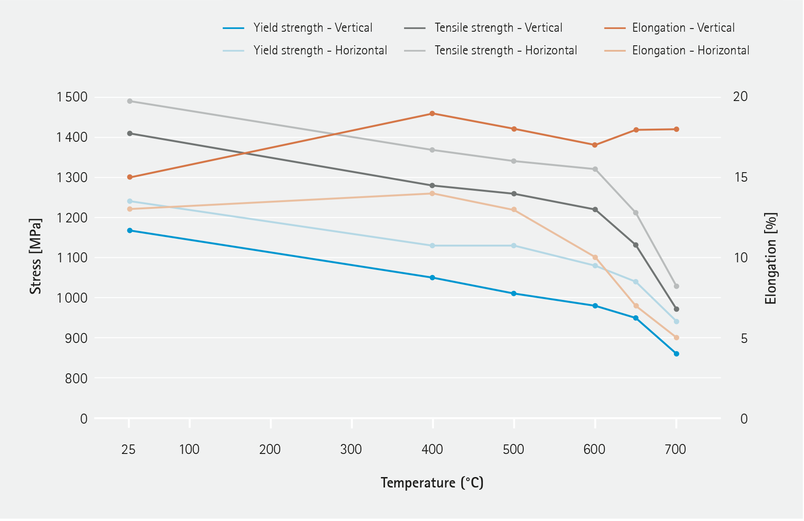
| Vertical | 1170 | 1410 | 15 | - | - | - |
| Horizontal | 1240 | 1490 | 13 | - | - | - |
Heat treatment procedure conform to Aerospace Material Specification AMS 2774 and AMS 5662.
As manufactured microstructure for additively manufactured IN718 consists of gamma phase (γ). Heat treatment for IN718 is required to produce desired microstructure and part properties (gamma double prime precipitates, γ"). Heat treatment is also used to relieve stresses.
Step 1:
Solution Anneal: hold at 954 °C (1750 °F ) for 1 hour per 25mm (0.98 inch) of thickness, air (/argon) cool
Step 2:
Ageing treatment; hold at 718 °C (1325 °F ) 8 hours, furnace cool to 621 °C (1150 °F ) and hold at 621 °C (1150 °F ) for total precipitation time of 18 hours, air (/argon) cool
Mechanical Properties As Manufactured
| EN ISO 6892-1 Room Temperature | 40 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 630 | 970 | 30 | - | - | - |
| Horizontal | 770 | 1060 | 26 | - | - | - |
Hardness
| EN ISO 6507 Heat Treated | |
|---|---|
| Value | 463 |
| Unit | HV |
| ASTM E292 Heat Treated | Stress [MPa] | Temperature [°C] | Time to Rupture [hrs] | Elongation [%] | RA [%] |
|---|---|---|---|---|---|
| Vertical | 689 | 650 | 53 | 5 | 20.05 |
The stress-rupture performance of EOS NickelAlloy IN718 was tested on vertically oriented samples, in heat-treated condition. No HIP was applied. The data presents the Larson-Miller parameter values achieved at stress levels of 689 MPa.
Surface Roughness
| Surface Roughness | From | To |
|---|---|---|
| Sa (µm) | - | - |
| Ra (µm) | - | - |
Process Information Metal
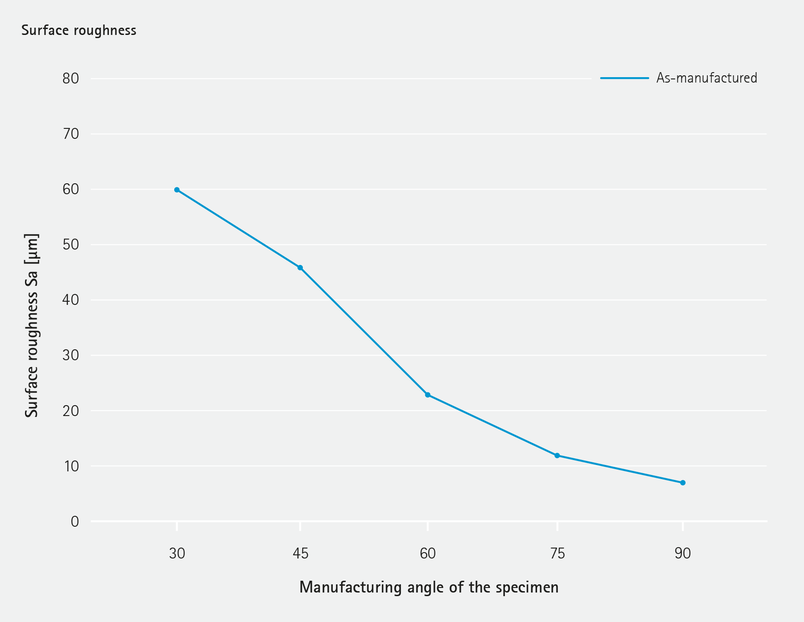
This process provides high productivity with a volume rate that is 119% faster than the IN718 40 µm Flexline and 77% faster than IN718 40 µm HiPro processes.
| System Setup | EOS M 400-4 |
|---|---|
| EOS Material set | IN718_040_080_HiProM404 |
| Powder Product No. | 9011-0020 / 9030-0022 |
| Software Requirements |
EOSPRINT 2.11 or newer |
| Recoater Blade | HSS (High Speed Steel) |
| Nozzle | EOS Aerospike Nozzle |
| Inert gas | Argon |
| Sieve | 63 µm |
| Additional Information | |
|---|---|
| Layer Thickness | 80 µm |
| Volume Rate | up to 4 x 9.2 mm³/s |
| Min. Wall Thickness | 0.3 - 0.4 mm |
Chemical and Physical Properties of Parts
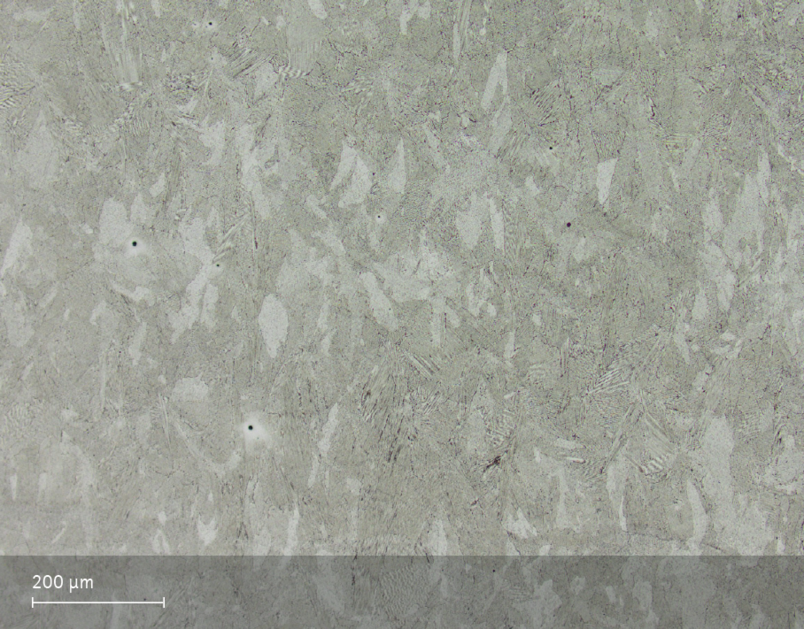
Microstructure of the Produced Parts
| Defects | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Defect Percentage | 80 µm | 0.025 % | - |
| Density EN ISO 3369 | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Density | 80 µm | ≥ 8.25 g/cm³ | - |
Mechanical Properties Heat Treated
| EN ISO 6892-1 Room Temperature | | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
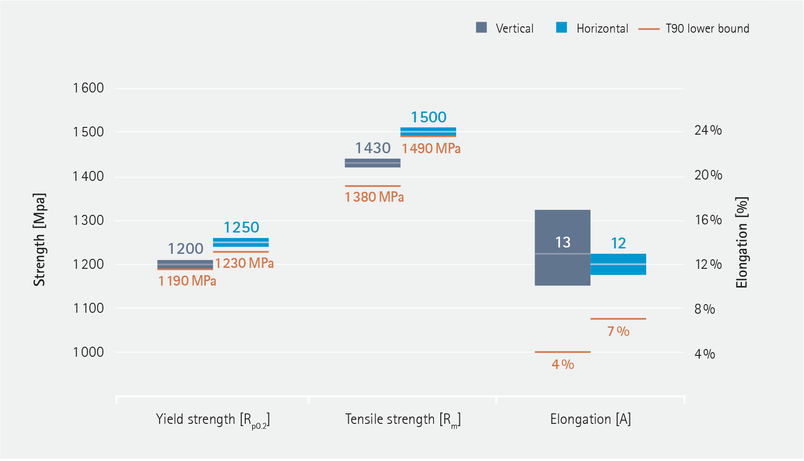
| Vertical | 1200 | 1430 | 13 | - | - | - |
| Horizontal | 1250 | 1500 | 12 | - | - | - |
Heat treatment procedure conform to Aerospace Material Specification AMS 2774 and AMS 5662.
As manufactured microstructure for additively manufactured IN718 consists of gamma phase (γ). Heat treatment for IN718 is required to produce desired microstructure and part properties (gamma double prime precipitates, γ"). Heat treatment is also used to relieve stresses.
Step 1:
Solution Anneal: hold at 954 °C (1750 °F ) for 1 hour per 25mm (0.98 inch) of thickness, air (/argon) cool
Step 2:
Ageing treatment; hold at 718 °C (1325 °F ) 8 hours, furnace cool to 621 °C (1150 °F ) and hold at 621 °C (1150 °F ) for total precipitation time of 18 hours, air (/argon) cool
Mechanical Properties As Manufactured
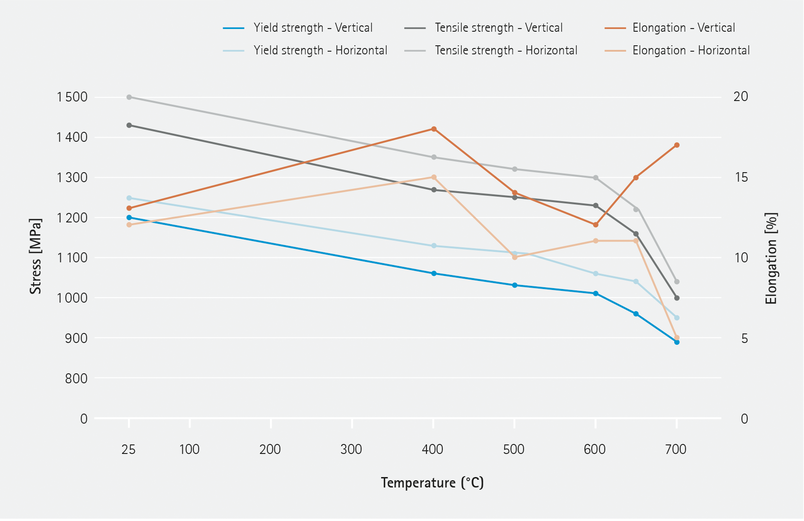
| EN ISO 6892-1 Room Temperature | 80 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 630 | 980 | 29 | - | - | - |
| Horizontal | 750 | 1060 | 25 | - | - | - |
| ASTM E292 Heat Treated | Stress [MPa] | Temperature [°C] | Time to Rupture [hrs] | Elongation [%] | RA [%] |
|---|---|---|---|---|---|
| Vertical | 689 | 650 | 56 | 9 | 20.07 |
The stress-rupture performance of EOS NickelAlloy IN718 was tested on vertically oriented samples, in heat-treated condition. No HIP was applied. The data presents the Larson-Miller parameter values achieved at stress levels of 689 MPa.
Surface Roughness
| Surface Roughness | From | To |
|---|---|---|
| Sa (µm) | - | - |
| Ra (µm) | - | - |
Process Information Metal
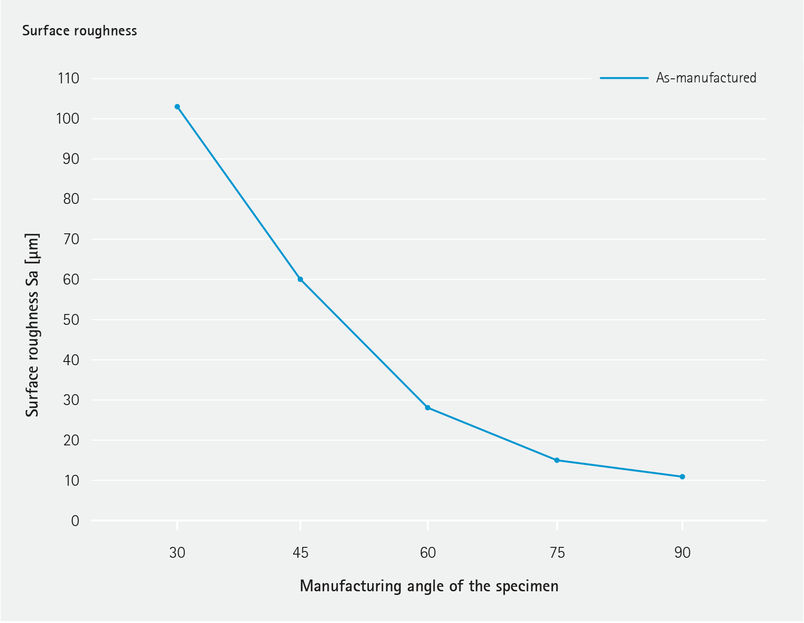
The material set enables processing of EOS NickelAlloy IN718 in 40 μm and 80 μm layer thicknesses using argon as inert gas. This set is a major overhaul of IN718_040_080_HiProM291 1.03 with new exposure options with improved low angle buildability and changed 40 μm exposure.
The exposure sets included are:
“EOS_Part” is the classic 40 μm set familiar from IN718_040_PerformanceM291 2.13. Full datasheet available here.
“EOS_Part_Fast” is the 80 μm set familiar from IN718_040_080_HiProM291 1.03.
“EOS_Part_LowAngle” presents a new exposure set with highly improved buildability of low angles with good surface roughness in 40 μm.
“EOS_Part_Fast_LowAngle” presents a new exposure set with highly improved buildability of low angles with good surface roughness in 80 μm.
| System Setup | EOS M 290 |
|---|---|
| Powder Product No. | 9011-0020 / 9030-0022 |
| Recoater Blade | HSS (High Speed Steel) |
| Nozzle | EOS Grid Nozzle |
| Inert gas | Argon |
| Sieve | 63 µm |
| Additional Information | |
|---|---|
| Layer Thickness | 40 um, 80 µm |
| Volume Rate | 4.6 / 8.2 mm³/s |
| Min. Wall Thickness | Typical 0.3 - 0.4 mm mm |
Chemical and Physical Properties of Parts
Microstructure of the Produced Parts
| Defects | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Defect Percentage | 40 µm | 0.01 % | - |
| Average Defect Percentage | 80 µm | 0.03 % | - |
| Density EN ISO 3369 | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Density | 40 µm | ≥ 8.15 g/cm³ | - |
| Density EN ISO 3369 | Thickness | Result | Number of Samples |
|---|---|---|---|
| Average Density | 80 µm | ≥ 8.15 g/cm³ | - |
Mechanical Properties
Mechanical Properties Heat Treated
| EN ISO 6892-1 Room Temperature | 40 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 1190 | 1390 | 15 | - | - | - |
| Horizontal | 1270 | 1530 | 17 | - | - | - |
The data has been generated with the exposure set "EOS_Part_LowAngle". See release note for details.
Heat treatment procedure conform to Aerospace Material Specification AMS 2774 and AMS 5662.
As manufactured microstructure for additively manufactured IN718 consists of gamma phase (γ). Heat treatment for IN718 is required to produce desired microstructure and part properties (gamma double prime precipitates, γ"). Heat treatment is also used to relieve stresses.
Step 1:
Solution Anneal: hold at 954 °C (1750 °F ) for 1 hour per 25mm (0.98 inch) of thickness, air (/argon) cool
Step 2:
Ageing treatment; hold at 718 °C (1325 °F ) 8 hours, furnace cool to 621 °C (1150 °F ) and hold at 621 °C (1150 °F ) for total precipitation time of 18 hours, air (/argon) cool
Mechanical Properties As Manufactured
| EN ISO 6892-1 Room Temperature | 40 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 660 | 970 | 33 | - | - | - |
| Horizontal | 190 | 170 | 27 | - | - | - |
The data has been generated with the exposure set "EOS_Part_LowAngle". See release note for details.
Mechanical Properties Heat Treated
| EN ISO 6892-1 Method A, Range 1 (0.00007 1/s) Room Temperature | 80 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 1200 | 1440 | 16 | - | - | - |
| Horizontal | 1230 | 1490 | 14 | - | - | - |
The data has been generated with the exposure set "EOS_Part_Fast_LowAngle". See release note for details.
Heat treatment procedure conform to Aerospace Material Specification AMS 2774 and AMS 5662.
As manufactured microstructure for additively manufactured IN718 consists of gamma phase (γ). Heat treatment for IN718 is required to produce desired microstructure and part properties (gamma double prime precipitates, γ"). Heat treatment is also used to relieve stresses.
Step 1:
Solution Anneal: hold at 954 °C (1750 °F ) for 1 hour per 25mm (0.98 inch) of thickness, air (/argon) cool
Step 2:
Ageing treatment; hold at 718 °C (1325 °F ) 8 hours, furnace cool to 621 °C (1150 °F ) and hold at 621 °C (1150 °F ) for total precipitation time of 18 hours, air (/argon) cool
Mechanical Properties As Manufactured
| EN ISO 6892-1 Method A, Range 1 (0.00007 1/s) Room Temperature | 80 µm | Yield Strength [MPa] | Tensile Strength [MPa] | Elongation at Break A [%] | Reduction of Area Z [%] | Modulus of elasticity [GPa] | Number of Samples |
|---|---|---|---|---|---|---|
| Vertical | 640 | 980 | 32.5 | - | - | - |
| Horizontal | 740 | 1040 | 29 | - | - | - |
The data has been generated with the exposure set "EOS_Part_Fast_LowAngle". See release note for details.
Surface Roughness
| Surface Roughness | From | To |
|---|---|---|
| Sa (µm) | - | - |
| Ra (µm) | - | - |